PSA Carbon Monoxide Purification
Carbon Monoxide Separation and Purification Technology
Carbon monoxide (CO), as an important C1 chemical feedstock, is used in the production of methanol, acetic acid, ethylene glycol, and other chemical products. Industrial CO-rich gas sources are diverse, including various coal gases (such as water gas and semi-water gas), cracking gases (from methanol or calcium carbide), off-gases (from yellow phosphorus or acetic acid production), as well as blast furnace gas and converter gas. Leveraging proprietary adsorbents,Lirun Technology has developed a dedicated CO separation technology capable of treating feed gases with high N₂/CH₄ content to achieve high-purity CO extraction.
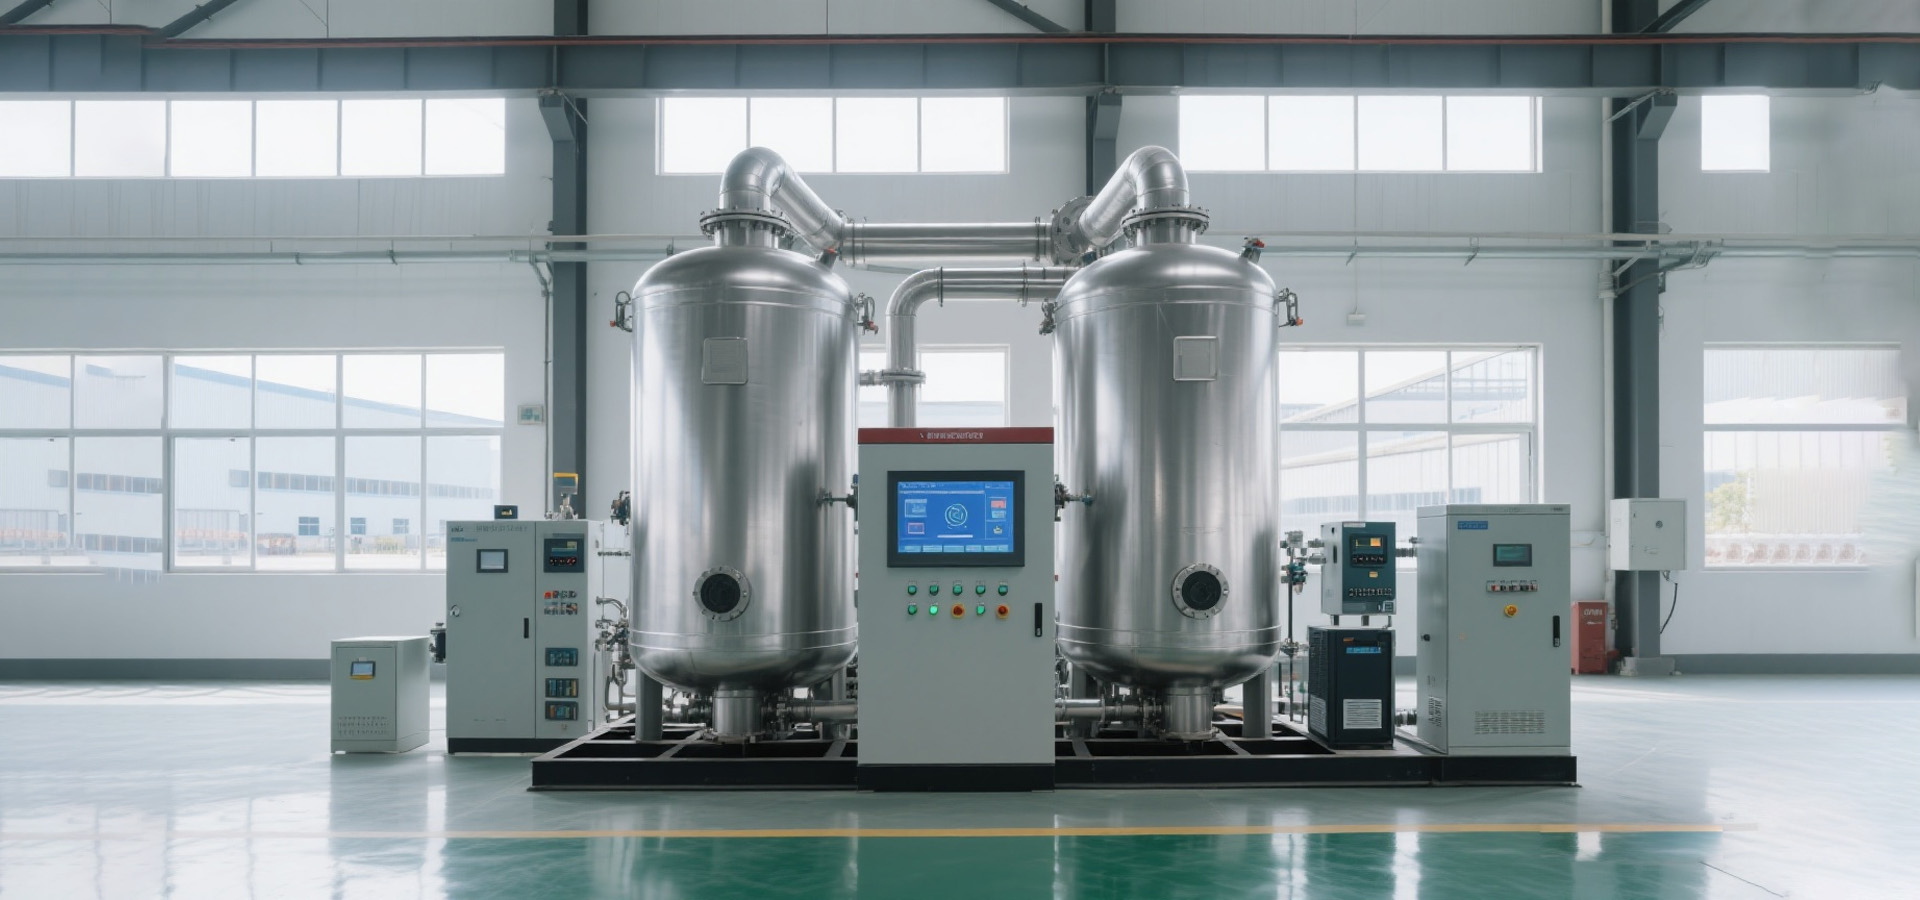
Two-Stage PSA Process
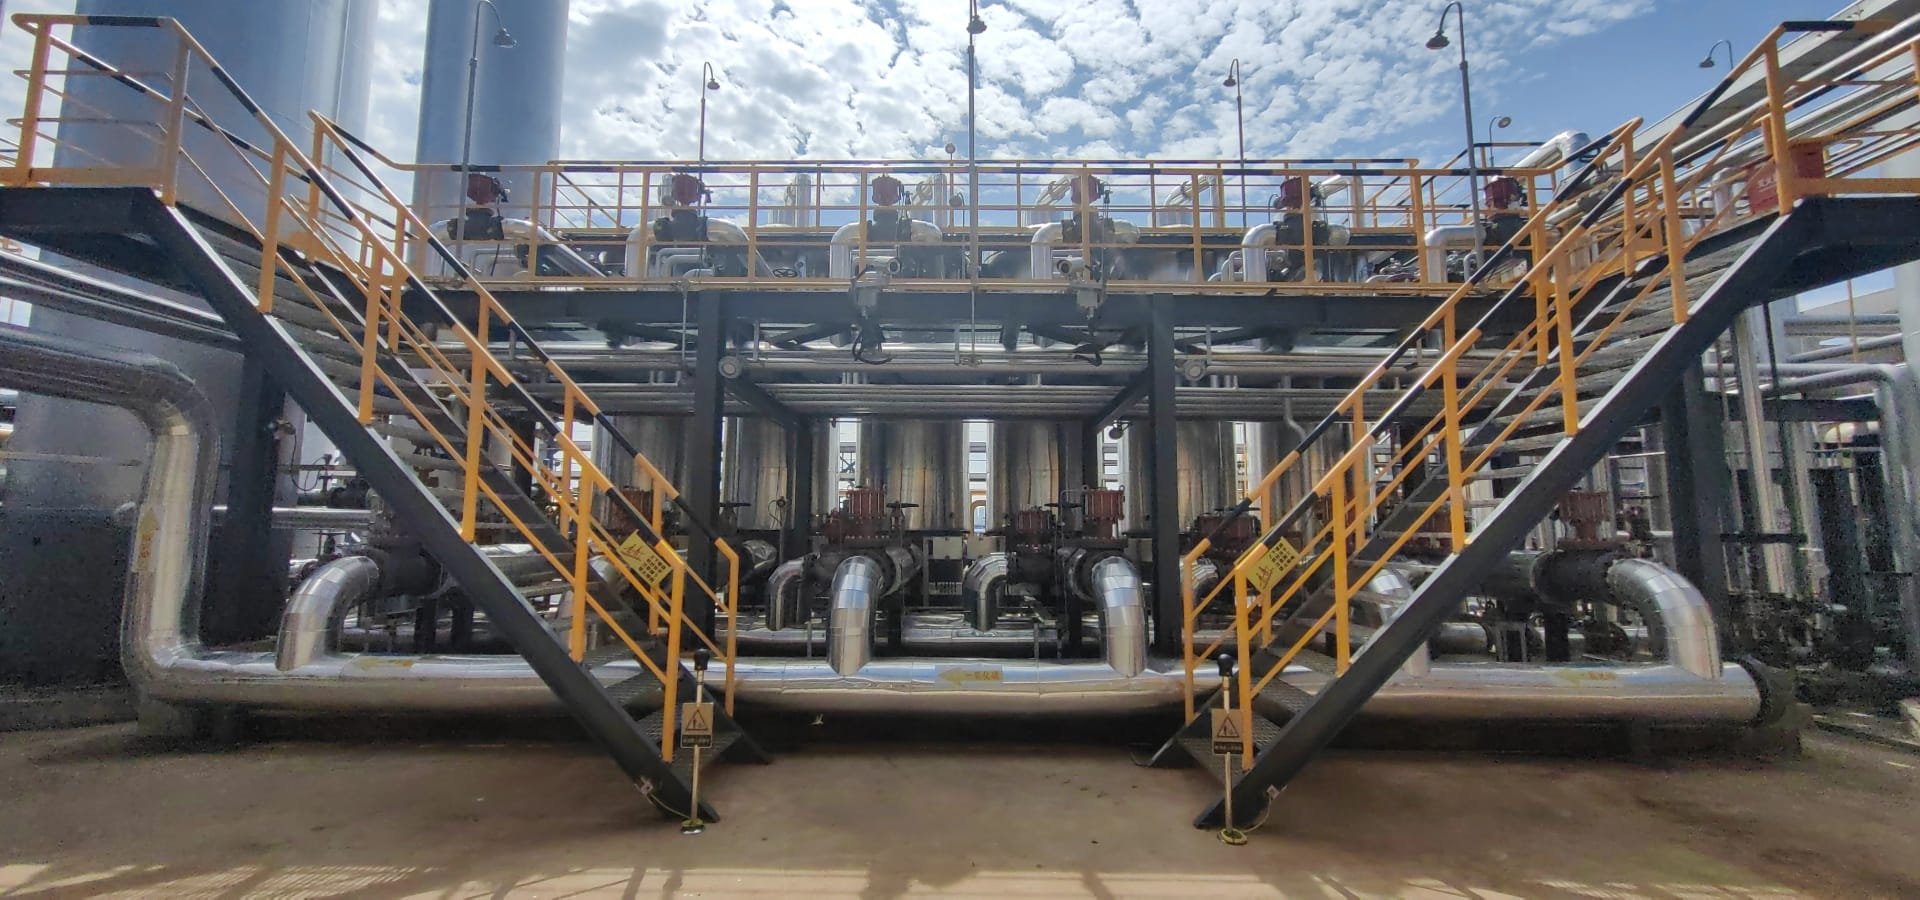
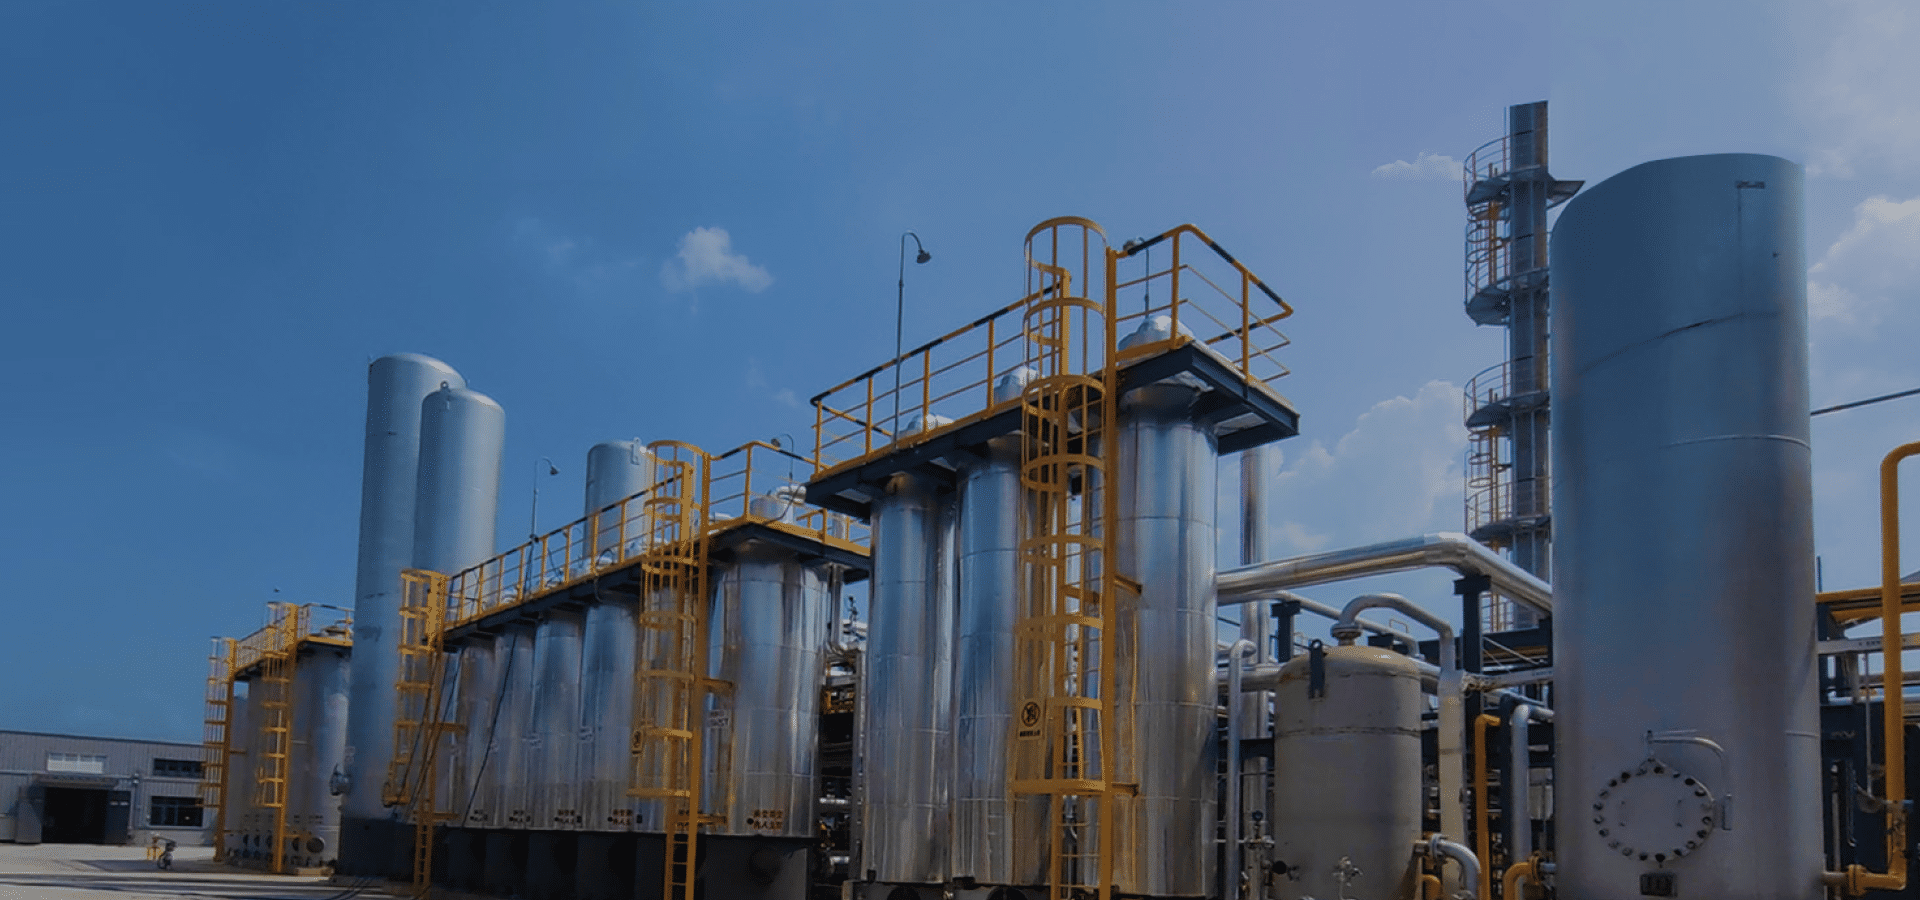
The process employs PSA-1 to remove acidic gases (CO₂, H₂S, etc.) and PSA-2 for deep purification of CO. Lirun Technology's self-developed copper-based adsorbents produce CO product gas with a purity of 98% (up to 99.9%) and a recovery rate of 80–95%.
Carbon Monoxide Separation and Purification Technology
Carbon monoxide (CO), as an important C1
chemical feedstock, is used in the production of methanol, acetic acid,
ethylene glycol, and other chemical products. Industrial CO-rich gas sources
are diverse, including various coal gases (such as water gas and semi-water
gas), cracking gases (from methanol or calcium carbide), off-gases (from yellow
phosphorus or acetic acid production), as well as blast furnace gas and
converter gas. Leveraging proprietary adsorbents,Lirun Technology has
developed a dedicated CO separation technology capable of treating
feed gases with high N₂/CH₄ content to achieve high-purity CO extraction.
Two-Stage PSA Process
The process employs PSA-1 to remove
acidic gases (CO₂, H₂S, etc.) and PSA-2 for deep purification of CO. Lirun
Technology's self-developed copper-based adsorbents produce CO product gas with a purity of 98% (up to
99.9%) and a recovery rate of 80–95%.